Industrial Concrete Coating
Industrial floors take a beating that would destroy an ordinary coating, forklifts, dropped tools, chemical spills, thermal shock, and round-the-clock traffic. GP Concrete Coatings installs industrial-grade systems built to absorb that punishment and keep performing.
Coatings That Survive the Plant Floor
A professionally installed industrial floor coating helps create a safer, cleaner, and more efficient workspace while extending the lifespan of the underlying concrete. By forming a durable protective barrier, the coating reduces surface wear, minimizes dust, and improves resistance to spills, moisture, and daily operational stress.
Beyond protecting the concrete, industrial coatings can help streamline facility maintenance and reduce costly disruptions caused by damaged flooring. Their seamless, non-porous surface makes routine cleaning easier, helping businesses maintain a cleaner and more organized work environment while supporting workplace safety.
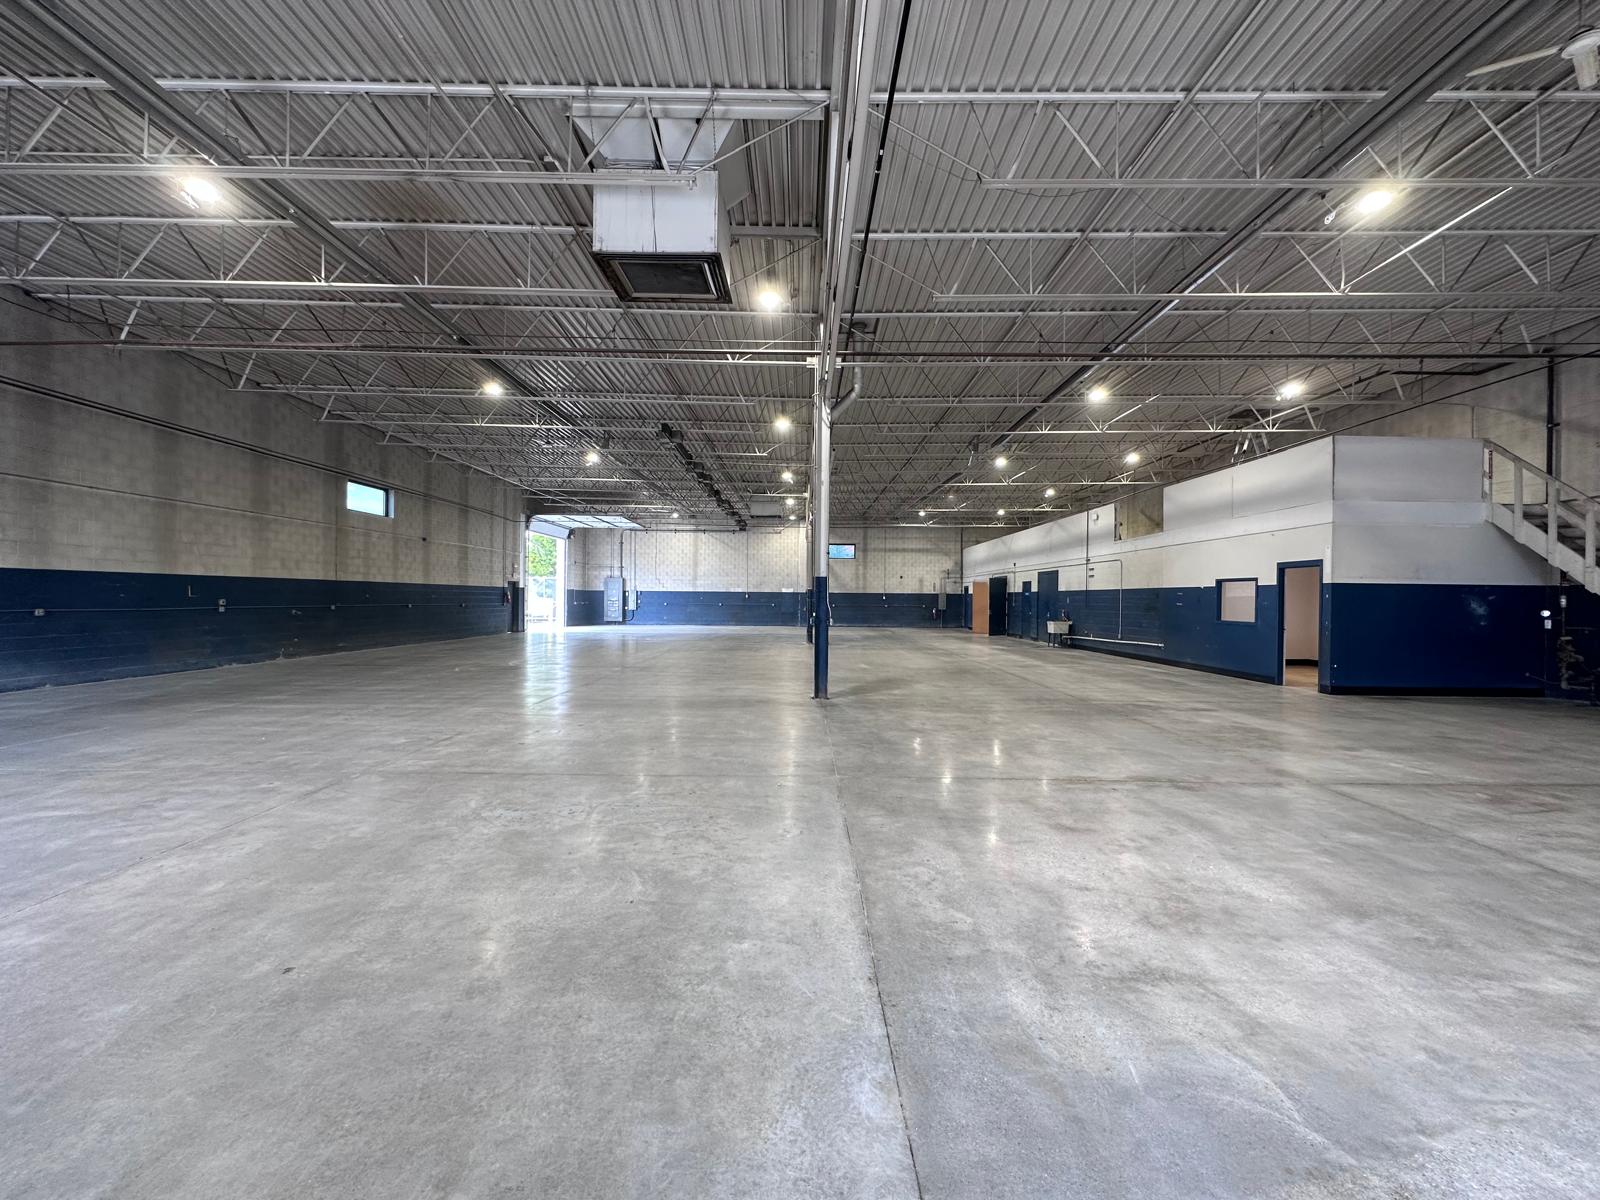
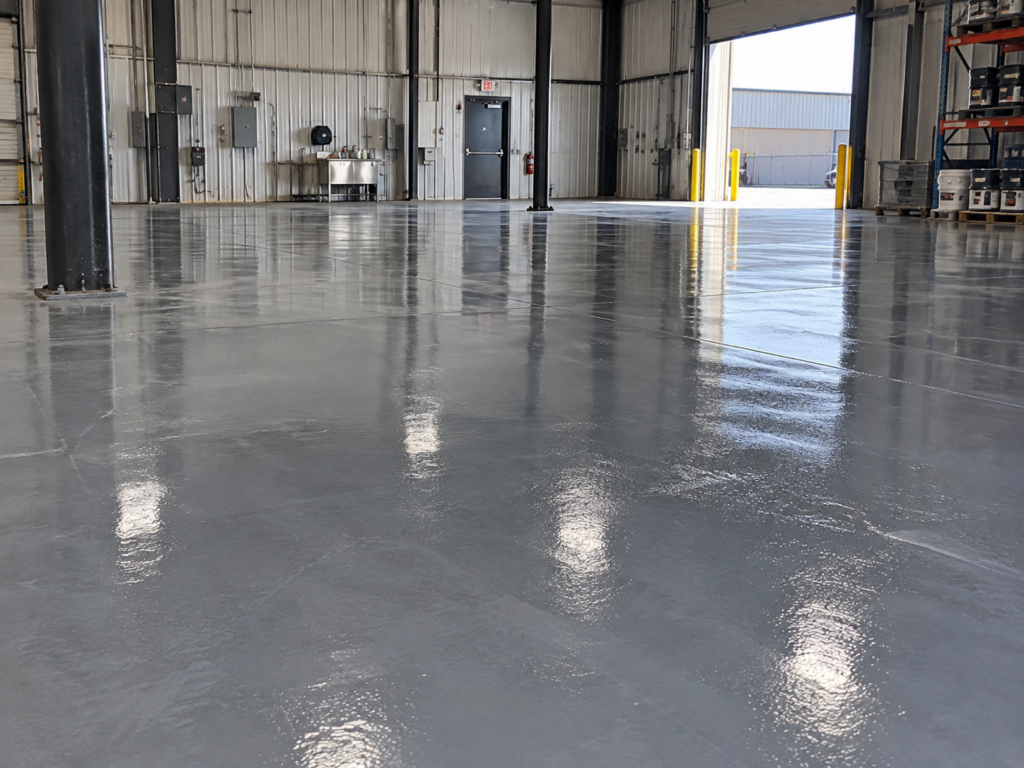
An industrial floor isn't just about durability, it's a safety system. We build in the features that keep your team protected and your facility compliant:
- Anti-slip aggregates calibrated to your environment and wet/dry conditions.
- High-visibility safety striping, walkways, and forklift lane markings.
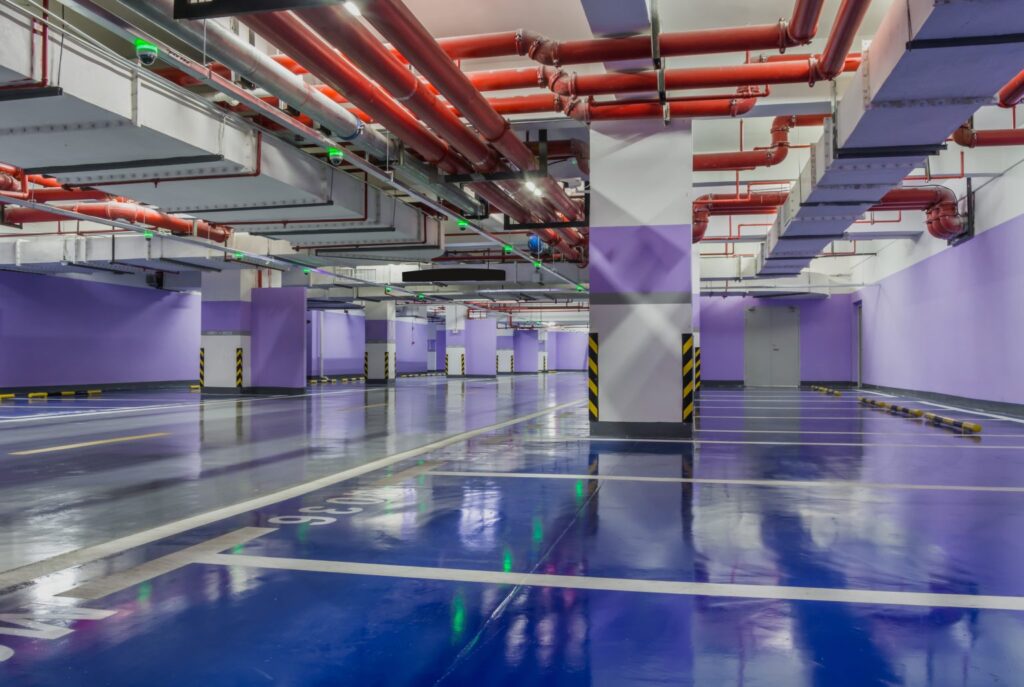
- Color-coded zones for storage, hazards, and equipment areas.
- Seamless surfaces that eliminate dust and bacteria-trapping cracks.
An industrial floor isn't just about durability, it's a safety system. We build in the features that keep your team protected and your facility compliant:
- Anti-slip aggregates calibrated to your environment and wet/dry conditions.
- High-visibility safety striping, walkways, and forklift lane markings.
- Color-coded zones for storage, hazards, and equipment areas.
- Seamless surfaces that eliminate dust and bacteria-trapping cracks.
Facilities We Coat

Warehouses &
distribution centers
Abrasion-resistant floors for racking, forklifts, and pallet jacks.

Manufacturing
plants
Durable surfaces that handle machinery loads and process spills.

Food & beverage processing
Seamless, sanitary, USDA-minded finishes that resist bacteria.

Warehousing
cold storage
Systems formulated to perform at low temperatures.
Why the Right Industrial Floor Coating Matters
Every facility has unique operational requirements, which is why there isn’t a one-size-fits-all flooring solution. Factors such as traffic volume, moisture levels, temperature fluctuations, chemical exposure, and cleaning procedures all influence which coating system will perform best. Proper evaluation and surface preparation are essential to achieving long-lasting adhesion and durability.
At GP Concrete Coatings, we assess the specific demands of your facility before recommending a flooring system. Whether you operate a manufacturing plant, warehouse, food processing facility, distribution center, automotive shop, or industrial workspace, our goal is to provide a flooring solution that delivers reliable performance for years to come.
Every facility has its own stresses. Here's how we engineer around the most common ones:
| Challenge | How We Solve It |
|---|---|
| Heavy forklift / vehicle traffic | High-build, impact-resistant systems that withstand point loads and constant wheeled traffic. |
| Chemical & oil exposure | Chemical-resistant coatings that protect the slab from solvents, acids, oils, and fuels. |
| Thermal shock & hot processes | Systems engineered to tolerate temperature swings, steam cleaning, and hot spills. |
| Moisture vapor in the slab | Moisture-mitigation primers that prevent delamination and bubbling. |
| Slip & safety compliance | Anti-slip aggregates and OSHA-aligned safety striping and zone markings. |
Explore Our Recent Work


Industrial facilities rely on us for high-performance concrete coating solutions that deliver exceptional durability, safety, and long-term protection. From thorough surface preparation to precision coating application, our team creates seamless, heavy-duty floors engineered to withstand constant forklift traffic, chemical exposure, impacts, abrasion, and demanding industrial environments.
Professional Surface Preparation
Heavy-Duty Industrial Coating Systems
Chemical & Abrasion Resistant Finishes
Experienced Industrial Installation Team
Long-Lasting, Low-Maintenance Protection

Frequently Asked Questions
What is industrial concrete coating?
Industrial concrete coating is a high-performance protective system applied to concrete floors to improve durability, resist heavy traffic, and protect against chemicals, abrasion, and daily wear.
Which industries benefit from industrial concrete coatings?
Industrial concrete coatings are commonly used in manufacturing plants, warehouses, distribution centers, food processing facilities, automotive shops, aircraft hangars, laboratories, and production facilities.
Can industrial coatings withstand forklift traffic?
Yes. Many industrial coating systems are designed to handle frequent forklift traffic, pallet jacks, heavy machinery, and other industrial equipment when properly installed.
Are industrial concrete coatings resistant to chemicals?
Yes. Depending on the coating system selected, industrial floors can offer excellent resistance to oils, fuels, solvents, cleaning chemicals, and many industrial liquids.
How important is surface preparation before coating?
Surface preparation is one of the most critical parts of the installation process. Proper grinding, cleaning, and repair help ensure strong adhesion and long-term coating performance.
Can damaged concrete floors be coated?
Yes. Minor cracks, pits, and surface imperfections are typically repaired before the coating system is installed to create a durable, long-lasting finish.
Are industrial concrete coatings easy to maintain?
Yes. Coated floors are easier to clean than untreated concrete because they create a seamless surface that reduces dust buildup and helps resist stains.
Can industrial floor coatings improve workplace safety?
Yes. Many coating systems include slip-resistant textures that can improve traction in wet or high-traffic areas while creating a brighter, cleaner work environment.